WorkshopMate Machining Centre
Turning Centre
Configure turning operations, tooling and cutting conditions from one engineering workspace.
1Inputs
Selected material
316
Stainless steel
ConditionAs supplied
Hardness150 HB
Tensile strength519 MPa
Machinability73% · Good
Coolant
Flood coolant or HP coolant for chip control
Chip control
Work hardens; use sharp geometry, positive cutting action, good coolant.
Machining notes
General starting point; confirm actual certificate/hardness.
Needs validation against supplier/toolmaker data
2Tool & insert
OD turning
RecommendedDCMT 11T304
General-purpose positive turning tool for finishing and light roughing.
55° diamond
HolderSDJCR 2020K11
InsertDCMT 11T304
GradeISO M25
Tool materialCarbide
CoatingCVD coated
Nose radius0.4 mm
Lead angle93°
Maximum DOC2.5 mm
Recommended setupKeep below 1.5 × holder height
- Suitable for profiling and shoulder turning.
- Use a larger nose radius for heavier roughing.
- Reduce overhang where chatter is present.
3Results
4Recommendations
Cutting conditions
OD turning on 316 at 150 m/min and 0.20 mm/rev.
- Operation
- OD turning
- Material
- 316
- Cutting speed
- 150 m/min
- Feed
- 0.20 mm/rev
- Depth of cut
- 1.5 mm
Tool setup
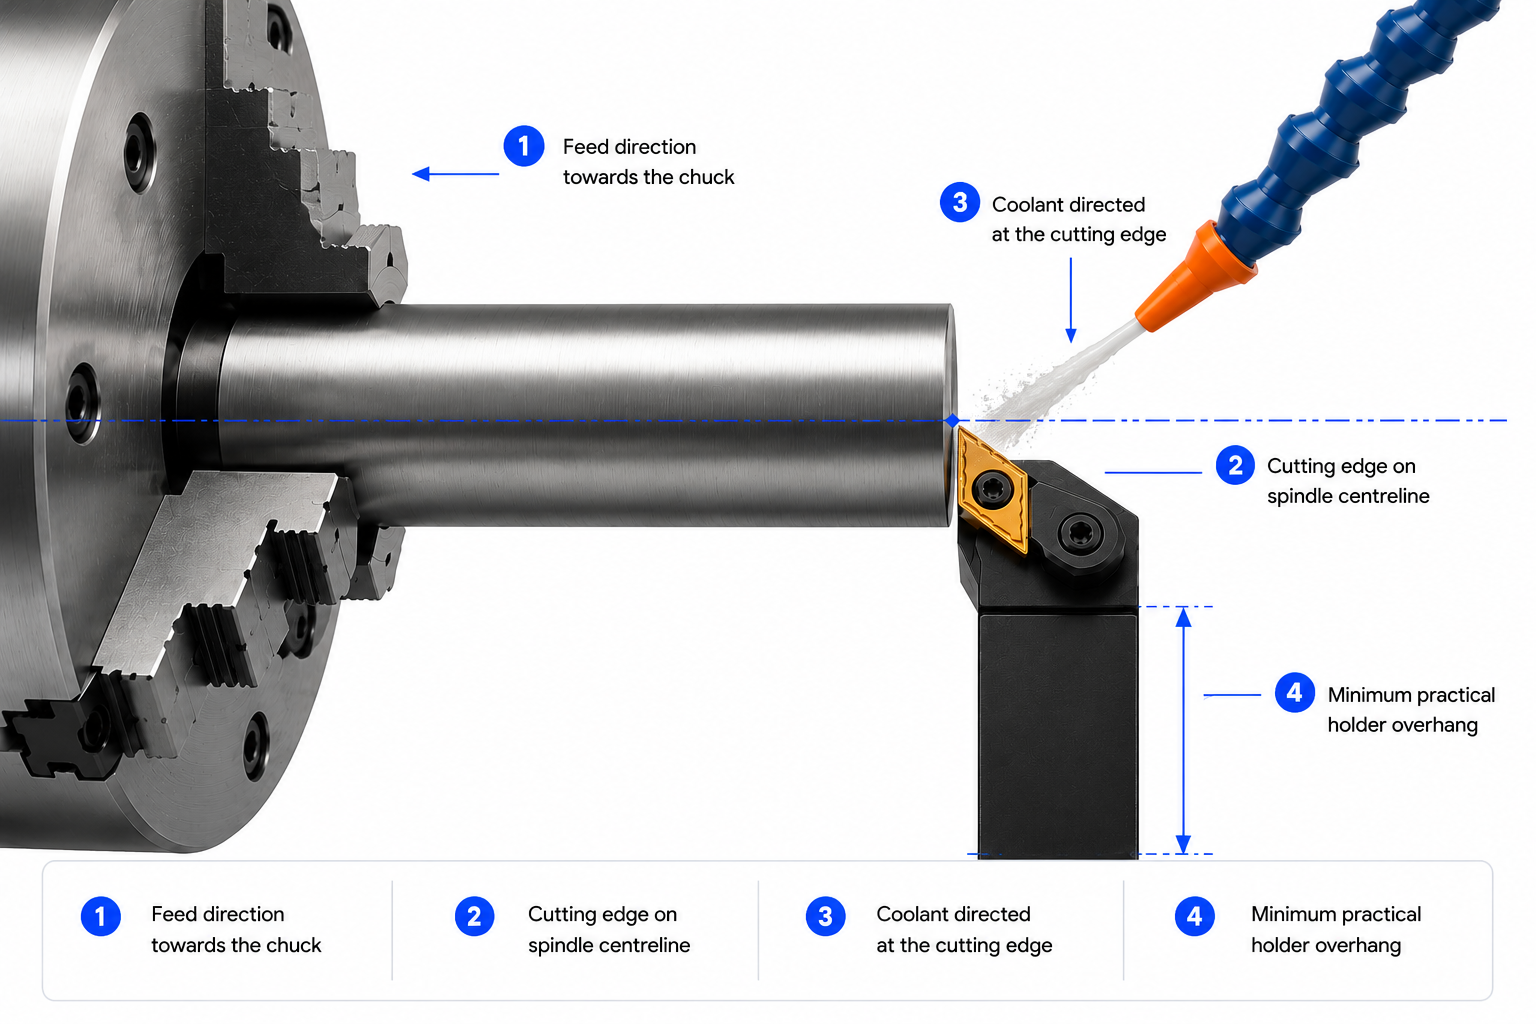
Recommended setup
Rigid and correctly aligned
- Keep the tool and workholding rigid.
- Minimise holder overhang.
- Verify the cutting edge is on centre height.
- Confirm the insert is seated and clamped correctly.
- Direct coolant at the cutting edge.
Setup statusRecommended
G-code example
G96 S150 M03
G95
G00 X52.0 Z2.0
G01 X50.0 F0.20
Troubleshooting
Chatter
Reduce overhang, check rigidity and lower cutting speed if required.
Poor surface finish
Check insert wear, nose radius, feed and coolant delivery.
Built-up edge
Increase cutting speed cautiously and confirm the insert grade suits the material.